
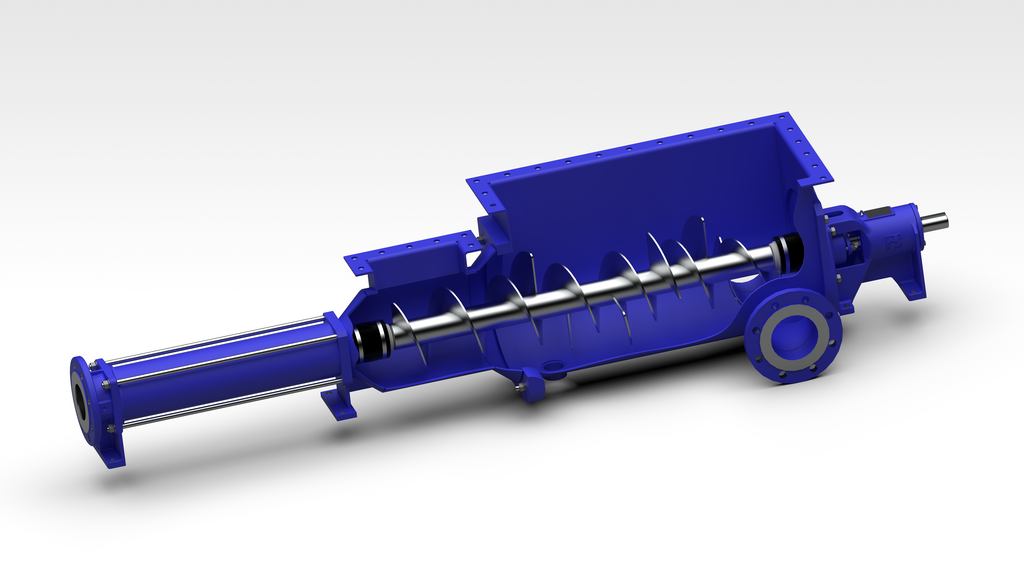
Closed-Pipe Conveying for the Toughest, Non-Flowing Media
Launched in 2026, the Allweiler AE-RD/RE is a progressing cavity hopper pump built for media that conventional pumps and conveyor screws struggle with: dewatered sewage sludge, thick pastes and other highly viscous, high-solids products. By moving these products through a closed pipeline instead of open conveyor belts, it reduces spillage and contamination and keeps the work area cleaner.
An optimised anti-bridging auger and vertical hopper walls keep material flowing into the pump without a separately driven bridge breaker, and the hopper can double as a storage buffer. A flow-optimised stuffing box between the hopper and rotor/stator fills the conveying chambers almost completely, protecting against partial dry running and reducing rotor and stator wear. The pump can also blend in chemicals or additives during pumping and can feed dryers and other downstream equipment directly at higher pressures than a conveyor screw.
Key Data
- Flow rate up to 1,000 l/min
- Differential pressure up to 24 bar
- Fluid temperature up to 135°C
- Solids content up to 85%, dry substance up to 35%
- Viscosity up to 850,000 mPas
Options for Maximum Uptime
- Maintenance in Place (MiP) design – change wear parts without removing the pump from the pipeline
- ALLDUR® long-life stators and hard-chrome plated ductile rotors
- Flushing connections and inspection openings in the hopper and stuffing box
- Adjustable hopper length to suit the feed situation
Suited for: wastewater and sludge treatment, paper, chemical and process engineering, marine, mining and power generation.


Reviews
There are no reviews yet.